Reliable Industrial Flow Control: Exploring the Best Valve Manufacturers in India
Flow control is a crucial aspect of industrial operations, influencing productivity, equipment safety, and overall system performance. Industries that handle water, oil, gas, chemicals, steam, and other fluids depend on reliable valves to maintain smooth and controlled operations. Selecting suitable valves helps minimize leakage risks, improve process efficiency, and support the long-term performance of industrial equipment.
India's growing manufacturing and infrastructure sectors have increased the demand for dependable flow-control solutions. Today, Valve Manufacturers in India serve a wide range of industries by offering products designed for different pressure ratings, temperatures, pipeline sizes, and operating environments.
Among the most widely used products are butterfly valves and ball valves. Each type offers distinct advantages, making it important for buyers to understand their functions before choosing a suitable solution. This guide explores the benefits, applications, and selection criteria associated with these essential industrial valves.
The Growing Importance of Industrial Valve Manufacturers
Industrial valves are more than simple pipeline components. They help control fluid movement, isolate equipment, support maintenance activities, and maintain the operating conditions required by industrial processes.
Reliable Valve Manufacturers combine engineering expertise, suitable raw materials, precise manufacturing methods, and quality inspections to produce products that meet specific requirements. Depending on the application, valves may be manufactured from stainless steel, carbon steel, cast iron, ductile iron, or other suitable materials.
When choosing a manufacturer, industrial buyers should consider product quality, design capabilities, testing procedures, compliance with relevant standards, and technical support. These factors can influence the valve's durability, maintenance requirements, and overall operating cost.
A well-selected valve can help improve system reliability and reduce interruptions caused by unsuitable materials, incorrect specifications, or premature component failure.
Butterfly Valve Manufacturers in India for Versatile Applications
Butterfly valves are widely used in industrial pipelines because of their compact construction and efficient operating mechanism. They contain a disc mounted on a rotating shaft within the valve body. As the disc turns, it changes the flow passage, allowing the valve to regulate or stop fluid movement.
Butterfly Valve Manufacturers in India provide different designs to meet the requirements of industries such as water treatment, infrastructure, power generation, chemical processing, and manufacturing.
Key Advantages of Butterfly Valves
Compact and lightweight construction
Butterfly valves generally occupy less space than many alternative valve arrangements. Their compact structure can simplify installation in pipelines with limited space.
Convenient operation
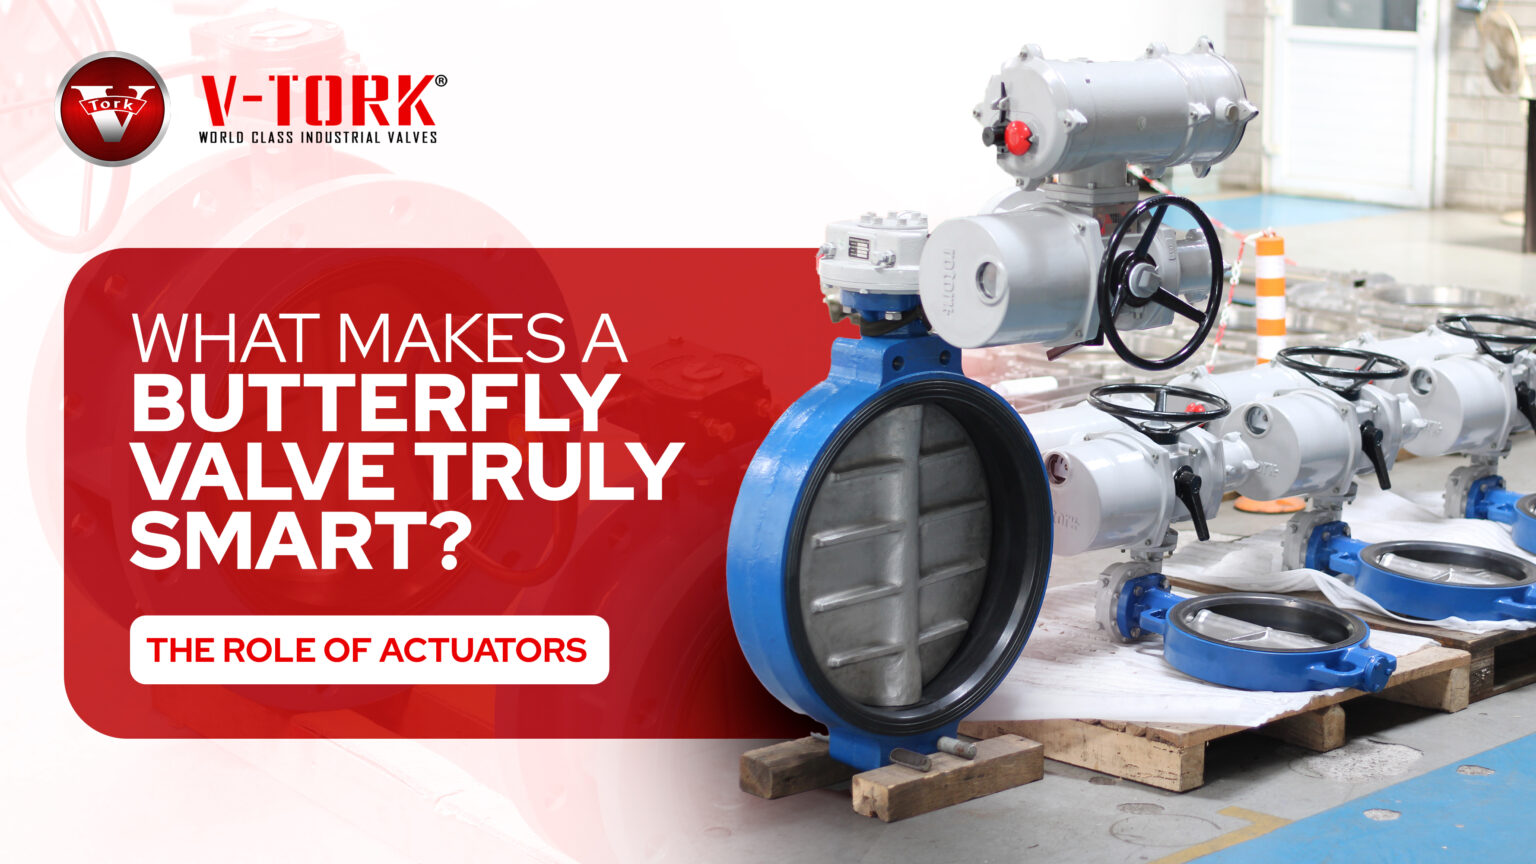
Most butterfly valves operate through a quarter-turn mechanism. Depending on the valve design and size, operation can be manual or automated using suitable actuators.
Economical flow control
For many large-diameter pipeline applications, butterfly valves offer a cost-effective solution. The final choice depends on operating pressure, material requirements, and service conditions.
Flexible configurations
Butterfly valves are available in wafer, lug, and flanged designs. Different body, disc, and seat materials allow manufacturers to address a wide range of applications.
Integration with automated systems
Electric and pneumatic actuators can be used with compatible butterfly valves to support remote operation and automated process control.
Industries That Use Butterfly Valves
Butterfly valves are commonly installed in:
- Water supply and distribution networks
- Wastewater treatment facilities
- HVAC and building services
- Industrial cooling-water systems
- Power generation plants
- Chemical and process industries
- Food and beverage manufacturing
When comparing Butterfly Valve Manufacturers in India, buyers should assess the valve's pressure and temperature ratings, sealing performance, material compatibility, connection type, and relevant testing documentation.
The selected valve should match the actual operating conditions rather than simply the pipeline dimensions or purchase budget.
Ball Valve Manufacturers in India for Dependable Shut-Off Solutions
Ball valves are an important choice for applications that require effective isolation and straightforward operation. These valves contain a spherical ball with a central bore. When the bore aligns with the pipeline, fluid can pass through. Turning the ball approximately 90 degrees closes the passage.
Ball Valve Manufacturers in India supply products for a variety of industrial applications, including water systems, oil and gas facilities, chemical plants, compressed-air networks, and general manufacturing.
Benefits of Ball Valves
Effective shut-off capability
Properly specified ball valves can provide reliable isolation, helping prevent unwanted flow through a pipeline.
Fast operation
The quarter-turn operating mechanism allows convenient opening and closing, making ball valves suitable for many on-off applications.
Efficient flow passage
A full-port ball valve provides a relatively unrestricted passage when fully open, which can help reduce pressure loss across the valve.
Different construction options
Manufacturers offer floating ball valves, trunnion-mounted ball valves, and different body designs to meet specific operating requirements.
Wide material selection
Depending on the intended service, ball valves may be available in stainless steel, carbon steel, brass, and other suitable materials, with compatible sealing components.
Applications of Ball Valves
Ball valves are widely used in petroleum refineries, oil and gas processing, chemical manufacturing, pharmaceutical facilities, industrial water systems, compressed-air installations, and other process industries.
The correct valve depends on the fluid, operating pressure, temperature, sealing requirements, and frequency of operation. For demanding applications, buyers should verify the manufacturer's specifications, testing records, and compliance with relevant project standards.
Choosing products from experienced Ball Valve Manufacturers in India can help businesses find suitable solutions for their operational needs.
How to Choose Between Butterfly Valves and Ball Valves
Selecting the right valve requires an understanding of the intended function and the system's operating conditions.
Butterfly valves are often preferred for larger pipelines, water distribution systems, and applications where compact construction and economical flow management are important. Ball valves are commonly selected for isolation duties that require effective shut-off and low flow resistance when fully open.
Before making a decision, consider these factors:
- System requirements: Determine whether the valve is needed for isolation, flow regulation, or another specific function.
- Pressure and temperature: Confirm that the selected design can safely handle the required operating range.
- Fluid compatibility: Choose suitable body, disc or ball, and seat materials for the fluid being transported.
- Pipeline configuration: Check the valve size, end connections, installation space, and maintenance access.
- Automation needs: Consider whether manual operation is sufficient or an actuator is necessary.
- Long-term operating costs: Evaluate maintenance, spare parts, service life, and replacement expenses alongside the initial price.
A detailed technical assessment helps avoid choosing a valve that is unsuitable for the intended application.
Essential Qualities of Trusted Valve Manufacturers
Finding the right manufacturer can make a significant difference in the performance and reliability of industrial systems. Buyers should evaluate suppliers using clear technical and commercial criteria.
1. Strong Manufacturing Capabilities
Look for manufacturers with experience in the required valve category and the ability to meet the specified dimensions, materials, pressure ratings, and connection requirements.
2. Consistent Quality Assurance
Ask about raw-material inspection, dimensional checks, pressure testing, and seat leakage testing. Relevant documentation should be available where required.
3. Compliance with Applicable Standards
Verify whether the products meet the specifications required by the project. Depending on the application, standards such as API, ASME, or ISO may be relevant.
4. Technical Expertise
A knowledgeable supplier should be able to clarify product specifications and provide guidance on valve selection, operating conditions, and installation requirements.
5. Reliable Supply and After-Sales Service
Product availability, realistic delivery schedules, spare parts, and responsive technical support are important considerations for industrial buyers.
6. Competitive Overall Value
A lower purchase price does not necessarily mean lower long-term costs. Durable construction, suitable materials, and reliable performance can help reduce maintenance expenses and unplanned downtime.
The Future of Industrial Valve Solutions in India
As industrial infrastructure expands, the demand for reliable flow-control products continues to evolve. Water management, energy production, chemical processing, and manufacturing all require valves that meet increasingly specific operating and performance requirements.
Developments in automated operation, improved sealing systems, corrosion-resistant materials, and quality-control methods are helping manufacturers address changing industry needs.
For industrial buyers, this creates opportunities to compare products and identify solutions tailored to their applications. However, reviewing technical specifications and verifying supplier capabilities remain essential steps in the procurement process.
Conclusion
Choosing suitable industrial valves is essential for maintaining efficient pipeline operations, reducing maintenance challenges, and supporting workplace safety. Experienced Valve Manufacturers can help businesses identify products that match their technical requirements and operating environments.
Butterfly valves offer practical solutions for many large-pipeline and water-management applications, while ball valves are widely valued for their convenient operation and dependable shut-off capabilities.
Businesses searching for Butterfly Valve Manufacturers in India or Ball Valve Manufacturers in India should focus on product quality, material compatibility, pressure ratings, testing procedures, applicable standards, and after-sales support.
By evaluating these factors carefully, companies can select reliable valve solutions that contribute to efficient industrial processes and long-term operational performance.


Comments
Post a Comment